
Contact Fumei
No.20 Jiuqiao Road, Shijiang Industrial Area, Jiujiang Town, Nanhai District, Foshan City, China.
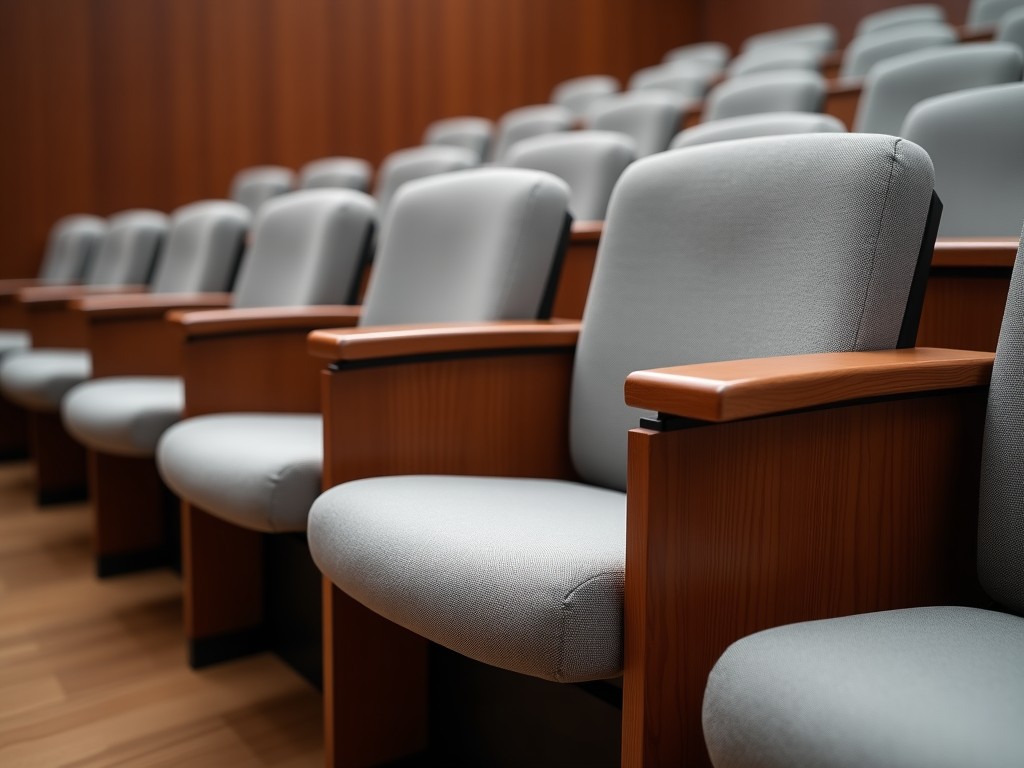
MC-02 steel classroom chairs. Featuring 1.2mm cold-rolled steel, 60kg/m³ molded foam, and 100k Martindale fabric. Ideal for university hall. OEM project supply.
Auditorium seating requires a precise balance of ergonomic support, structural durability, and aesthetic integration within large-volume spaces. Manufacturers supplying modern chairs for these environments must address long-term wear from high-cycle use, varying occupant anthropometrics, and acoustic performance considerations. OEM partnerships allow clients to specify chair geometry, material finishes, and mounting systems while leveraging the manufacturer’s production infrastructure and quality systems.
This page outlines the technical framework for sourcing auditorium chairs from a Chinese manufacturer offering OEM services, focusing on design parameters, material specifications, customization workflows, and validation methods relevant to institutional procurement. Each section explains functional requirements before detailing how they are addressed in the product offering.
Seat depth typically ranges from 450mm to 500mm to accommodate thigh support without impeding circulation. Backrest height is generally set between 900mm and 1050mm from the seat surface to provide lumbar and upper thoracic support. Seat width per person is standardized at 500mm–550mm in contiguous rows, accounting for shoulder breadth and clothing bulk. These dimensions are derived from ISO 9241-5 and ANSI/HFES 100-2007 guidelines for public seating.
Recline angle is usually fixed between 95° and 105° relative to the seat plane to maintain pelvic stability while allowing slight posterior tilt. Armrest height, when present, aligns with elbow height at 200–250mm above the seat, reducing shoulder elevation. Footprint depth per chair, including knee clearance, ranges from 750mm to 850mm depending on row spacing and egress requirements.
Frame construction commonly uses cold-rolled steel tubing with a minimum wall thickness of 1.2mm for the seat and back support structures, providing a yield strength exceeding 250 MPa. Leg assemblies often incorporate oval or rectangular sections to resist torsional loading under dynamic loads. Joints are typically welded using MIG/TIG processes with penetration verification to ensure load path integrity under 1100N dynamic seat load tests (per BIFMA X5.1).
Seat and back cushions utilize molded polyurethane foam with a density range of 40–60 kg/m³ for the seating surface and 30–45 kg/m³ for the backrest, offering a compression set below 5% after 80,000 cycles. Upholstery materials include polyester-coated fabrics with abrasion resistance exceeding 100,000 Martindale cycles and flame retardancy compliant with CAL 117 or EN 1021-1/2. Optional veneer or laminate finishes on exposed panels use E1-rated substrates with UV-stable surface coatings.
The OEM process begins with technical specification alignment, where clients provide dimensional constraints, load requirements, finish preferences, and integration points (e.g., power/data ports, ganging mechanisms). Manufacturers respond with preliminary 3D models and material datasheets for review. Iterative feedback cycles adjust ergonomic contours, mounting hardware, and accessory integration before tooling finalization.
Prototype validation includes static load testing (150% of rated load for 1 minute), cyclic durability (60,000–120,000 cycles depending on application), and flame spread assessment. Tooling is released only after documented compliance with client-specified performance thresholds. Production batches undergo incoming material inspection, in-process weld checks, and final assembly audits per AQL 1.0 standards.
Lead times typically range from 8–12 weeks for tooling and first article approval, followed by 4–6 weeks per 500-unit production batch, depending on finish complexity and order volume. Clients receive batch-specific test reports, material certificates, and assembly drawings upon shipment.
Frame integrity is verified using ultrasonic testing on critical welds and load-deflection mapping under 1100N dynamic seat load (simulating 50th percentile male occupant shifting). Load is applied via standardized hemispherical pads to replicate real-world pressure distribution. Acceptable deflection is limited to 8mm under load with full recovery within 5 seconds post-unload.
Fabric abrasion resistance is tested per ASTM D4966 (Martindale) with endpoint defined as two yarn breaks or noticeable performance change. Flame resistance is assessed via vertical flame test (ASTM D6413) with afterflame limited to 2.0 seconds and char length under 75mm. Foam indentation load deflection (ILD) is measured at 25%, 50%, and 65% compression to confirm load-bearing consistency across production lots.
Final inspection includes dimensional verification of seat height (±5mm), backrest angle (±1°), and ganging alignment (±2mm over 10 chairs). Packaging integrity is validated through drop testing (ISTA 1A) and vibration simulation to ensure damage-free transit. All test records are retained for traceability and supplied with shipment documentation.
| Component | Standard Option | Customizable Range |
|---|---|---|
| Seat Height | 450mm | 420mm–480mm |
| Backrest Height | 950mm | 900mm–1050mm |
| Frame Material | Cold-rolled steel (SPCC) | Stainless steel 304, aluminum alloy 6063 |
| Upholstery | Polyester fabric, 100k Martindale | Vinyl, wool blend, flame-retardant trevira |
| Armrest | Fixed, polyurethane | Optional, adjustable height, wood/metal inlay |
| Mounting | Floor-fixed, bracket | Retractable, beam-mounted, freestanding |
Values represent typical configurations. Exact specifications are confirmed during OEM engineering review based on project requirements, load conditions, and regulatory frameworks.
In auditoriums, sightline integrity is critical; chair height and backset must be coordinated with tiered riser geometry to ensure unobstructed views to the stage or screen. A 100mm increase in seat height typically requires a 150–200mm increase in riser rise to maintain C-value (vertical sightline clearance) above 80mm. Manufacturers provide seating layout templates to assist architects in verifying vertical and horizontal sightlines during early design phases.
Acoustic performance is influenced by seat absorption coefficients; upholstered seats and backs typically provide NRC values between 0.40 and 0.60 depending on fabric porosity and foam open-cell content. This contributes to reverberation control in speech-critical environments without requiring excessive wall treatment. Fire safety compliance is addressed through material certification and aisle width adherence to local building codes (e.g., NFPA 101, IBC).
For multipurpose halls requiring rapid reconfiguration, chairs may incorporate folding mechanisms or caster-based mobility with locking casters rated for 150kg dynamic load. Gangable designs use interlocking brackets that maintain alignment under lateral loads while allowing tool-free separation. Storage density is optimized through nesting profiles that reduce footprint by 60% when stacked.








